- By ali-steel
- 21 Dec 2024
- Industrial Manufacturing
- No Comments
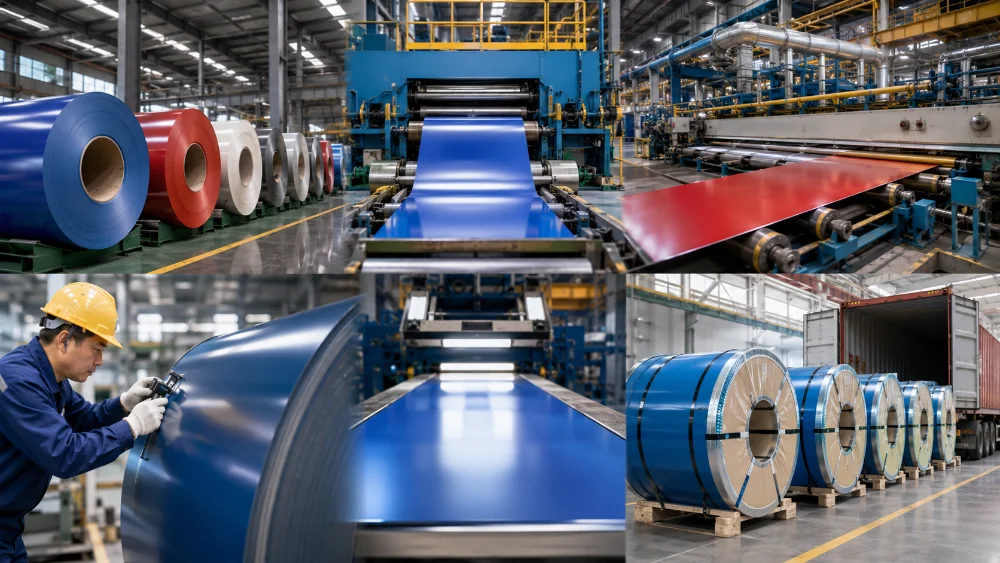
Prepainted galvanized iron, commonly known as PPGI, is widely used in roofing, wall cladding, sandwich panels, appliances, garage doors, storage systems, and industrial products.
Although PPGI is often described simply as painted galvanized steel, its manufacturing process involves several controlled stages.
The final quality depends on the steel substrate, metallic coating, cleaning process, pretreatment, primer, paint, curing, inspection, packaging, and delivery.
At Ali Steel, understanding the complete manufacturing process helps us guide customers toward products that meet their technical, visual, and commercial requirements.
What Is PPGI?
PPGI is galvanized steel that receives an organic paint coating before it is fabricated into the final product.
The word “prepainted” means the steel is painted in coil form before being transformed into roofing sheets, wall panels, appliance components, or other products.
The galvanized layer protects the steel from corrosion. The primer and topcoat add:
- Color
- Weather resistance
- Surface protection
- Gloss
- Texture
- Chemical resistance
- Improved appearance
PPGI is used in:
- Construction
- Roofing
- Wall cladding
- Appliances
- HVAC systems
- Transportation
- Industrial equipment
- Furniture
- Doors
- Prefabricated buildings
Step 1: Confirming Customer Requirements
The manufacturing process should begin with a clear understanding of the final application.
Important details include:
- Indoor or outdoor use
- Final product
- Project environment
- Required steel grade
- Thickness
- Width
- Coil weight
- Zinc coating
- Paint system
- Color
- Gloss
- Surface texture
- Forming requirements
- Applicable standards
- Packaging needs
- Transportation conditions
A PPGI coil used for roofing in a coastal area may require a different coating system from material used for indoor appliances.
At Ali Steel, customer requirements are reviewed before product selection so the supplied material matches its intended use.
Step 2: Selecting the Steel Substrate
The base steel determines strength, formability, flatness, and dimensional stability.
Different applications require different mechanical properties.
The substrate may be selected according to:
- Yield strength
- Tensile strength
- Elongation
- Surface condition
- Chemical composition
- Flatness
- Thickness tolerance
- Width tolerance
A steel grade suitable for rigid roofing sheets may not be the best option for deep drawing or complex forming.
Inconsistent substrate quality can cause cracking, poor forming, uneven profiles, or production difficulties.
Step 3: Applying the Zinc Coating
For standard PPGI, the steel is galvanized before painting.
In a continuous hot-dip galvanizing process, the steel strip passes through molten zinc. The zinc forms a metallic layer over the surface.
This coating protects the steel by:
- Creating a barrier
- Reducing direct exposure
- Providing sacrificial protection
- Improving corrosion resistance
The galvanizing process must control:
- Zinc coating mass
- Coating uniformity
- Surface appearance
- Adhesion
- Edge quality
- Spangle
- Strip flatness
Some prepainted products use alternative metallic coatings, including aluminum-zinc alloys.
The suitable metallic coating depends on environment, application, and required service life.
Step 4: Uncoiling the Material
The galvanized coil is placed on the coil-coating line using an uncoiler.
The strip is fed continuously into the production line.
The leading end of one coil may be joined to the end of another coil, allowing production to continue with minimal interruption.
Continuous processing improves consistency and helps maintain stable operating conditions.
Step 5: Cleaning the Surface
The galvanized surface may contain:
- Oil
- Dust
- Dirt
- Storage residues
- Processing contamination
The strip must be cleaned before pretreatment and painting.
Cleaning may include chemical washing, rinsing, and mechanical brushing.
This stage is critical because paint cannot develop reliable adhesion on a contaminated surface.
Inadequate cleaning may lead to:
- Peeling
- Poor adhesion
- Surface defects
- Blistering
- Uneven color
- Premature corrosion
The cleaning process must remove contamination without damaging the metallic coating.
Step 6: Chemical Pretreatment
After cleaning, the strip receives a chemical pretreatment.
Pretreatment improves the bond between the metallic surface and the primer. It may also enhance corrosion resistance.
The treatment must be:
- Uniform
- Compatible with the substrate
- Compatible with the primer
- Suitable for the paint system
- Properly dried
Poor pretreatment may not become visible immediately. Problems may appear later during bending, profiling, installation, or outdoor exposure.
Step 7: Primer Application
After pretreatment and drying, a primer is applied to the steel strip.
Primer supports:
- Paint adhesion
- Corrosion resistance
- Coating stability
- Forming performance
The primer may be applied to one or both sides.
The front side usually receives a complete decorative coating system. The reverse side may receive a back coat suitable for protection, insulation bonding, or another production requirement.
Primer thickness must remain consistent across the entire coil width.
Step 8: First Curing Stage
The primed strip passes through an oven.
The heat cures the primer and develops its intended mechanical and chemical properties.
Curing is more than simple drying.
The manufacturer must control:
- Oven temperature
- Strip temperature
- Line speed
- Residence time
- Cooling
Under-curing can cause poor adhesion or insufficient hardness. Over-curing may reduce flexibility or affect coating performance.
Step 9: Topcoat and Back-Coat Application
After the primer is cured and cooled, the topcoat is applied.
The topcoat provides:
- Final color
- Gloss
- Texture
- Ultraviolet resistance
- Weather protection
- Scratch resistance
- Chemical resistance
Common paint systems include:
- Polyester
- Silicone-modified polyester
- Polyurethane
- Plastisol
- PVDF
- Specialized industrial coatings
The reverse side may receive a different back coat depending on the final use.
The coating equipment must maintain uniform application throughout the coil.
At Ali Steel, coating specifications are reviewed according to the customer’s required appearance, environment, and performance expectations.
Step 10: Final Curing and Cooling
After topcoat application, the steel enters a second curing oven.
This stage develops the final properties of the coating.
The strip is then cooled before it touches rollers or is rewound.
Incorrect cooling can create:
- Surface marking
- Blocking
- Gloss variation
- Coating damage
- Uneven appearance
The line must maintain stable conditions to ensure consistent quality from the beginning to the end of the coil.
Step 11: Inspection and Quality Testing
Inspection takes place throughout production and before the finished coil is approved.
Tests may include:
- Steel thickness
- Zinc coating mass
- Paint thickness
- Color difference
- Gloss
- Adhesion
- Hardness
- Flexibility
- Impact resistance
- Bend testing
- Surface inspection
- Coil width
- Coil weight
- Edge quality
- Mechanical properties
Surface defects may include:
- Scratches
- Marks
- Uneven color
- Pinholes
- Bubbles
- Contamination
- Paint streaks
- Edge damage
Traceability is also important. Each coil should be connected to its production batch and inspection results.
Step 12: Recoiling and Conversion
After inspection, the finished strip is rewound into a coil.
Depending on the customer’s order, it may be:
- Supplied as a master coil
- Slit into narrower coils
- Cut into flat sheets
- Roll-formed into roofing sheets
- Converted into wall panels
- Laminated into sandwich panels
Every additional operation must be performed carefully to avoid scratches, edge damage, or paint cracking.
Step 13: Packaging
Packaging protects the finished product during handling, storage, and transportation.
The package should help prevent:
- Water entry
- Condensation
- Dust
- Surface scratches
- Coil movement
- Edge damage
- Impact
- Incorrect lifting
Labels should identify:
- Coil number
- Product specification
- Color
- Thickness
- Width
- Weight
- Batch number
- Customer order
Clear labeling reduces mistakes and supports traceability.
Step 14: Transportation and Final Delivery
Product quality can still be affected after manufacturing.
Incorrect transportation may cause:
- Coil movement
- Edge damage
- Water exposure
- Surface marks
- Deformation
- Packaging failure
The product should be secured correctly and protected from weather during transportation.
After delivery, coils and sheets should be stored in dry, ventilated conditions. Prolonged exposure to trapped moisture can damage even high-quality coated material.
At Ali Steel, dependable delivery and careful handling are treated as part of the complete product experience.
Conclusion
The PPGI manufacturing process is a carefully controlled sequence.
The steel substrate provides strength. The galvanized coating protects against corrosion. Pretreatment and primer support adhesion, while the topcoat provides color, appearance, and environmental resistance.
Quality also depends on inspection, traceability, packaging, transportation, and storage.
At Ali Steel, we focus on helping customers understand the complete product specification rather than comparing materials only by price or color. By combining suitable material selection with dependable supply and clear technical information, we support customers in choosing PPGI products that offer consistent performance and long-term value.


